A Provider of Smart Manufacturing and Services for Automated Control Valves
Empowering Automated Control Across Diverse Sectors
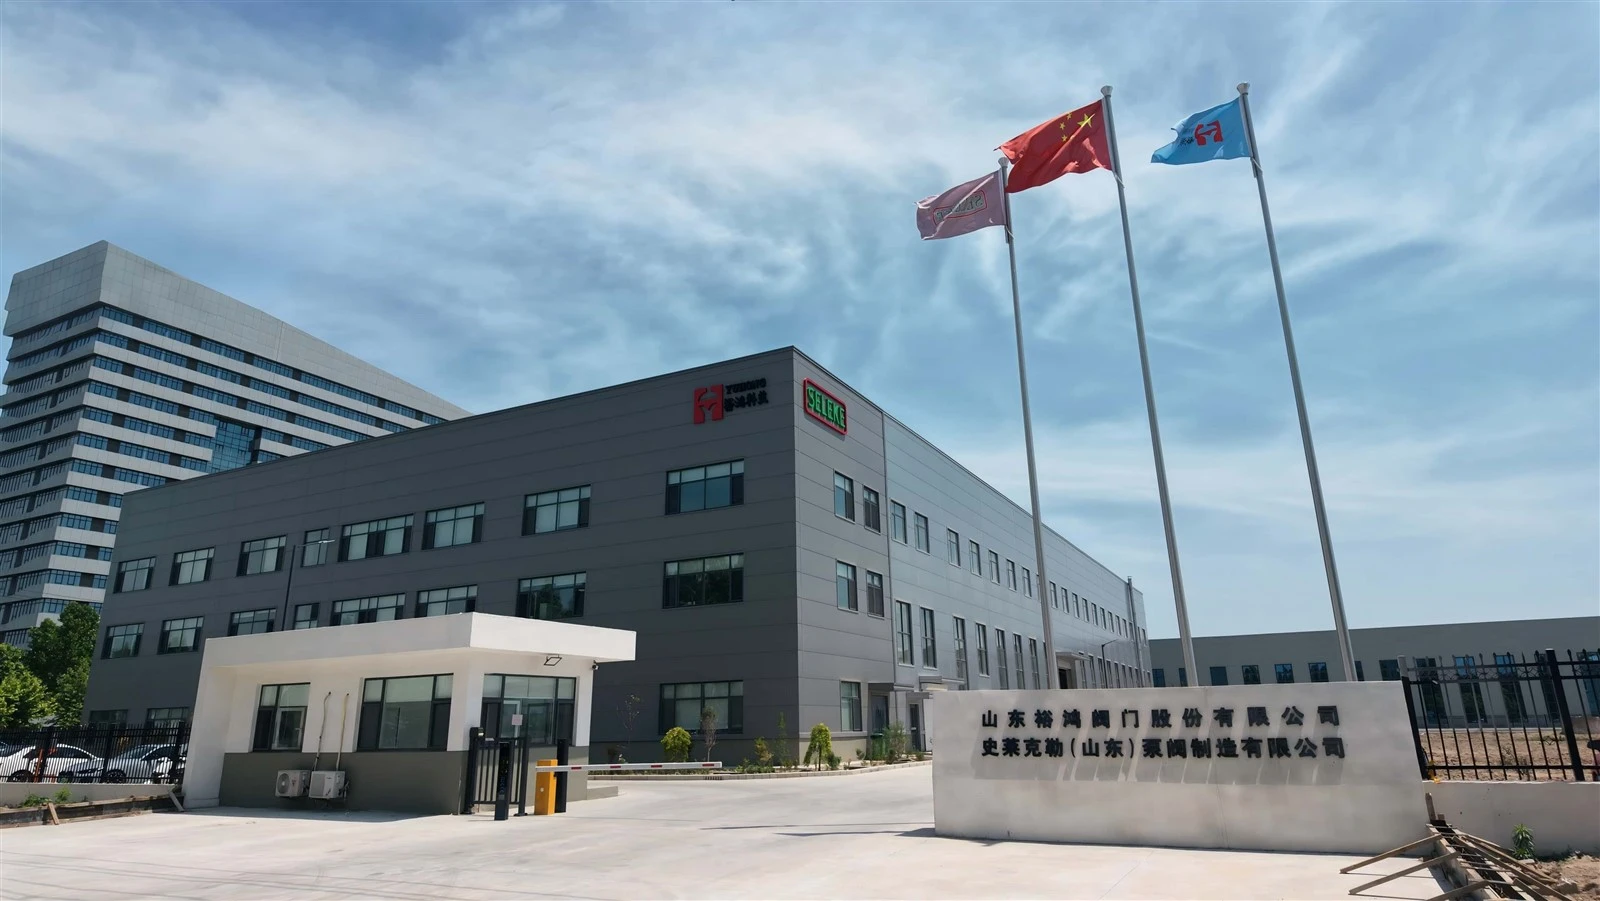
Established in February 2011 and based in Zibo, Shandong, Shandong Yuhong Valve Co., Ltd. is a high-tech enterprise-recognized as a "Specialized, Refined, Unique, and Innovative" (SRUI) enterprise-that integrates R&D, intelligent manufacturing, sales and service, technical exchange, and import-export trade. Long dedicated to the field of industrial fluid control, the company focuses on providing comprehensive valve solutions for automated industrial applications across various sectors.
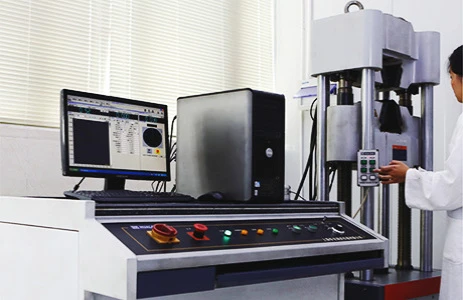
The company boasts robust infrastructure, with a brand-new, 40-mu (approx. 2.67-hectare) modern intelligent manufacturing facility that officially commenced production in October 2025. The workshop is equipped with over fifty precision machining units-including CNC machine tools, machining centers, and gantry milling machines-enabling the large-scale, precision manufacturing of valves for both general and specialized operating conditions, with a total annual capacity of 50,000 automated valve units. Yuhong operates its own standardized comprehensive testing laboratory, possessing full-spectrum testing capabilities-such as spectral analysis, material strength testing, physicochemical inspection, X-ray/magnetic particle/ultrasonic non-destructive testing, and valve type testing-to ensure rigorous quality control throughout the entire process, from raw material intake and component machining to the final shipment of finished products.
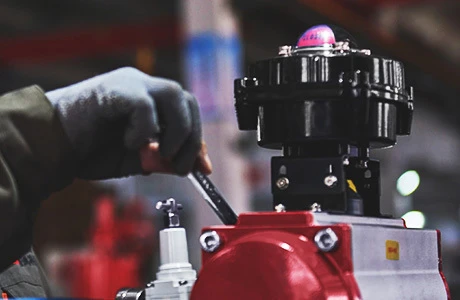
The company specializes in a full range of pneumatic and electric automated valves. Its core product portfolio includes control valves, ball valves, butterfly valves, solenoid valves, iris valves, guide vane valves, and pinch valves. These products come in comprehensive specifications and offer excellent adaptability to various operating conditions, meeting the demands for media regulation, shut-off, transport, and remote control in complex environments.
Yuhong's products are widely used in key sectors such as petrochemicals, crude oil extraction, natural gas transmission, fine refining, biopharmaceuticals, thermal power generation, metallurgy and mineral processing, papermaking and air separation, food and beverage brewing, municipal heating, and environmental sewage treatment. They reliably serve industrial automation production lines across these industries and have earned widespread recognition from upstream and downstream clients for their outstanding performance.
The company maintains a comprehensive standardized management system and has successfully obtained multiple authoritative certifications, including ISO9001 International Quality Management System certification, the Manufacturing License for Special Pressure Pipeline Components, TUV certification, and CE certification. Our products strictly adhere to national GB and HG industry standards and can also be custom-manufactured to meet international standards such as DIN (Germany), ANSI (USA), and JIS (Japan). The entire product line has passed certifications for explosion-proof and fire-safety capabilities, as well as other mandatory national inspections, ensuring comprehensive compliance and operational safety.
We are steadfastly committed to a development philosophy centered on quality and comprehensive service, upholding a corporate spirit of integrity, pragmatism, unity, and progress, while adhering to a business ethos that prioritizes the customer and fosters mutually beneficial partnerships. Rooted in our core business of valve manufacturing, we refine our products with craftsmanship and drive growth through innovation. Looking ahead, Shandong Yuhong Valve Co., Ltd. will continue to focus on the fluid control sector, deepening our expertise and forging ahead with determination. We look forward to joining hands with partners across the industry in sincere cooperation to shape a new landscape for the sector and create a brilliant future together.
Corporate Culture
Provide customers with products, services, and system solutions that meet their application needs.
Corporate Positioning
Domestic substitution
Precise selection
Customization as the blade
01
Enterprise Value
Supply customers' needs
Ensure stable production
02
Corporate Mission
Breaking through international technical barriers
Forging a national brand in the fluid control sector
03
Corporate Values
Service with Heart
Quality First
Win-Win for Long-Term Success
Innovation-Driven Development
04
Corporate Vision
A global pioneer across the entire fluid control value chain
05
Our Advantages
1. Solid backing from a team of professional engineers
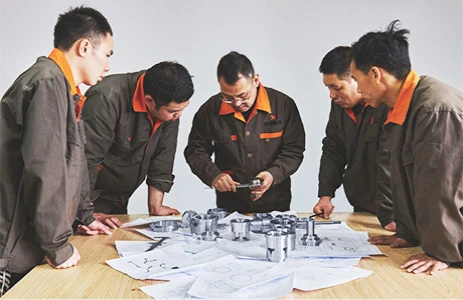
Our engineering team is our core strength; they possess not only extensive industry experience but also profound professional expertise in areas such as technical R&D, product design, and manufacturing. Their specialized knowledge and skills ensure our products maintain a significant market position, enabling us to provide customers with superior valve solutions.
Our engineering team is dynamic and innovative. They maintain a keen insight into new technologies, materials, and processes, continuously driving our product development and technological upgrades.
2. Rigorous quality management system
Our valve products undergo rigorous quality management throughout the entire process - from design and production to final dispatch. We maintain a comprehensive quality management system in which dedicated personnel oversee every stage - including raw material procurement, production process control, product inspection, and after-sales service - to ensure consistently high product quality.
Our quality management system guarantees not only the quality of our products but also the quality and efficiency of our services.
3. Advanced production equipment and technology
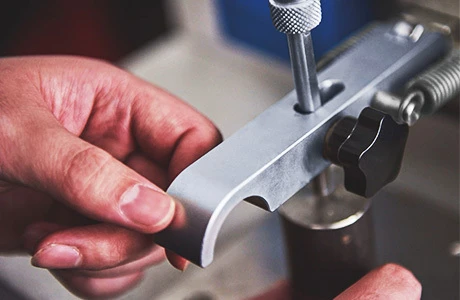
We possess advanced production equipment and technology, which are crucial to ensuring product quality and production efficiency. Our equipment is sourced from renowned domestic and international manufacturers and is characterized by high efficiency and stability. Our technical capabilities - spanning valve design, manufacturing processes, and testing - are at the forefront of the industry.
These advanced facilities and technologies enable us to consistently deliver products of high quality and superior performance.
4. Comprehensive after-sales service system
We maintain a comprehensive after-sales service system that provides customers with a one-stop service experience. Our services - ranging from product installation guidance and usage training to routine maintenance and troubleshooting - ensure that customers can use our products with confidence.
Our after-sales service system not only resolves issues encountered during product use but also enhances the operational efficiency and service life of our products.